#4 – 20133 102nd Avenue, Langley, B.C. V1M 4B4 Canada
#4 – 20133 102nd Avenue, Langley, B.C. V1M 4B4 Canada
Buying precision injection parts in 2026 requires more than comparing unit prices. Buyers must connect design intent, process capability, material behavior, and supplier reliability. A polished quotation can still hide weak inspection methods or unstable tooling. Look beyond the spreadsheet.
This guide introduces seven practical tips for evaluating precision injection suppliers with greater confidence. It examines tolerance control, mold maintenance, resin traceability, sampling procedures, and production documentation. It also considers newer tools, including digital quality records and automated visual inspection. These tools can improve visibility, but they do not replace experienced engineers examining a fresh sample under proper lighting.
A dependable supplier should explain how critical dimensions are measured, recorded, and corrected. Ask for capability data, inspection reports, and clear acceptance criteria. Request sample parts before approving large production volumes. Hold the part in your hand. Check its surface, fit, flash, warpage, and consistency across the batch.
Real purchasing decisions are rarely perfect. Drawings may change, forecasts may be optimistic, and a familiar supplier may miss an important detail. That is why precision injection sourcing needs documented evidence, open communication, and controlled verification. A low price may look attractive today, yet hidden rework can quickly erase the savings. These seven tips are designed to help buyers challenge assumptions, reduce avoidable risk, and select partners that can support stable production throughout 2026.
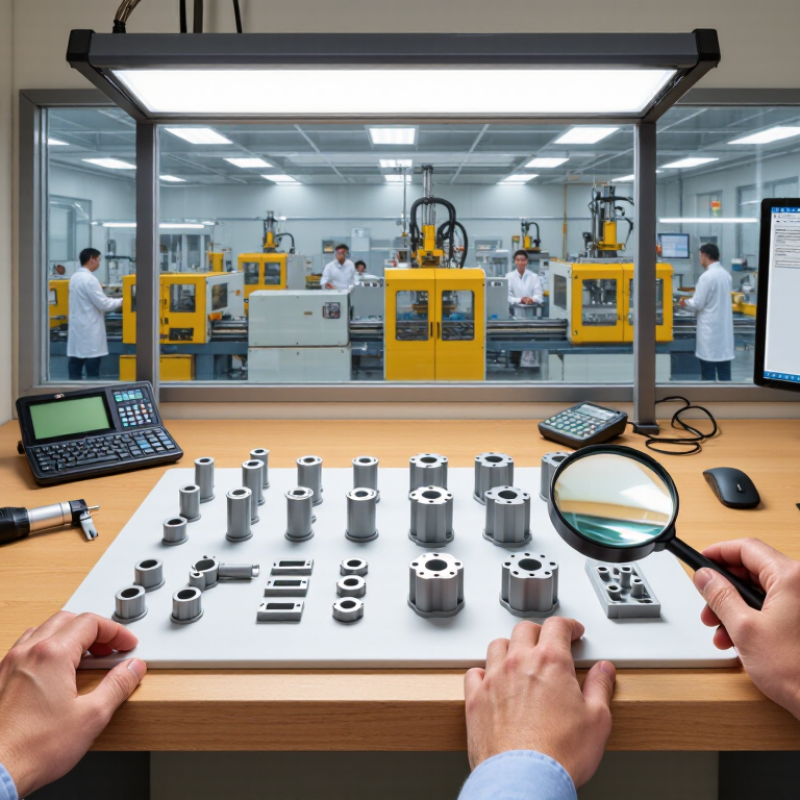
Precision injection molding uses controlled pressure, temperature, and cooling to produce repeatable plastic components. In 2026, buyers are applying it to medical housings, electric vehicle sensor covers, wearable devices, and microfluidic parts. These products often require tight tolerances, clean surfaces, and stable performance across thousands of cycles. A practical review should examine cavity balance, material behavior, shrinkage data, and inspection methods. Digital mold-flow analysis helps, but it cannot replace physical samples.
Tips
Experienced buyers also inspect process capability, commonly using Cpk data for important dimensions. A supplier should explain sampling frequency, gauge calibration, and corrective-action procedures clearly. Ask how the mold handles weld lines, sink marks, and warpage near ribs. Small design changes can prevent expensive tooling revisions later.
No process is perfect. Our early assumptions can be wrong. Recycled or filled materials may shift shrinkage and surface texture. That risk deserves testing, not optimistic language. A pilot run with measured parts, packed samples, and documented settings gives buyers stronger evidence than a polished presentation.
Before requesting a quote, describe what the part must do, not just how it looks. Include a dimensioned drawing, the latest revision, expected production volume, and the surfaces that mate with other components. Mark critical features clearly. A 0.2 mm variation may be harmless on a cover but disruptive at a snap-fit or sealing face. State how the part will be used, including temperature, load, and contact with moisture or chemicals. Small details matter.
Material selection should follow those conditions. A stiff resin can hold shape well, while a more flexible grade may survive repeated clips or impacts. Check the supplier’s data sheet for strength, shrinkage, and temperature limits, then discuss processing needs such as drying. Data sheets are useful, but they do not predict every result. Color, wall thickness, and flow direction can affect the finished part. Test the actual geometry.
Set tolerances around function and inspection capability. Avoid applying a tight tolerance to every dimension; it can raise tooling and measurement costs without improving performance. Identify datums and specify how key dimensions should be checked, such as with calipers or a fixture. In practice, teams sometimes overlook draft angles or uneven wall thickness until samples arrive. Review a prototype under real assembly conditions, and revise the drawing when it reveals an assumption that was wrong.
| # | Buyer Tip | Define in the Part Requirements | Material and Tolerance Guidance | What to Verify with the Supplier |
|---|---|---|---|---|
| 1 | Separate critical from non-critical dimensions | Identify dimensions that affect fit, sealing, alignment, safety, or function. Mark these clearly on the drawing and state the inspection method where necessary. | Apply tighter tolerances only to function-critical features. As an early planning reference, ordinary molded dimensions may require tolerances around ±0.2–0.5 mm, while selected precision features may target approximately ±0.05–0.10 mm when the material, geometry, tooling, and process support it. | Request a design-for-manufacturing review and confirmation that each proposed tolerance is achievable and measurable. Do not treat planning ranges as guaranteed limits. |
| 2 | Choose material by performance, not just price | Specify the required strength, stiffness, impact behavior, chemical exposure, operating temperature, appearance, and any regulatory or flammability requirements. | Material families differ in shrinkage and dimensional stability. Semi-crystalline polymers such as polypropylene and polyamide generally show more shrinkage-related movement than many amorphous polymers. Glass-fiber reinforcement can reduce shrinkage in some directions but increase directional variation. | Approve the exact resin grade and colorant, and ask for the material data sheet. Confirm that any proposed grade substitution has been evaluated against the part’s functional and compliance requirements. |
| 3 | Specify resin conditioning and moisture needs | State whether the part will be used dry, conditioned, or exposed to moisture, and define the state in which critical dimensions must be inspected. | Some materials, including many polyamides, absorb moisture and can change dimensions and mechanical properties as they condition. A measurement made immediately after molding may not represent the part’s dimensions in service. | Agree on drying, conditioning, storage, and inspection timing. Ask the supplier to document the condition of samples used for dimensional approval. |
| 4 | Design wall thickness and geometry for stability | Identify nominal wall thickness, transitions, ribs, bosses, and cosmetic surfaces. Avoid abrupt thickness changes where practical and include draft suitable for the part and tool. | Uneven or locally thick sections can contribute to sink, voids, warpage, and longer cooling time. Uniform walls and gradual transitions generally make filling and cooling easier, but the suitable thickness depends on the material, flow length, and part design. | Review wall-thickness analysis and proposed gate locations. Confirm that ribs and bosses are designed to limit sink and that the part can be ejected without damage. |
| 5 | Define datums and measurement conditions | Set a clear datum reference frame, identify inspection points, and specify units, temperature, and any conditioning period needed for reliable comparison. | Complex molded parts can flex or warp during measurement. A tolerance is only useful when the part is located and measured consistently, using a method appropriate to the feature and its function. | Agree on the coordinate measuring machine, gauges, fixtures, or other inspection method for critical features. Ensure supplier and buyer inspection plans use the same datum scheme. |
| 6 | Plan for shrinkage and warpage in tooling | Provide the final part geometry, material grade, assembly interfaces, and any surfaces where flatness, position, or alignment is especially important. | Tool dimensions are not a simple universal offset from the part dimensions. Shrinkage depends on resin, geometry, flow direction, processing conditions, and tool design; reinforced materials may shrink differently along and across the flow direction. | Ask how shrinkage assumptions will be validated and how first-article results will inform tool corrections. Review warpage risks before releasing production tooling. |
| 7 | Agree on validation and change control | Define sample quantities, required reports, acceptance criteria, approved material, and the process or tool changes that require prior approval. | First-article inspection and capability data can help determine whether critical dimensions are stable in production. A tolerance should be reviewed against actual process performance rather than accepted on paper alone. | Request documented first-article measurements and a control plan for critical features. Establish notification and approval requirements for changes to resin, tooling, process settings, or manufacturing location. |
Note: Tolerance figures are indicative planning ranges, not universal specifications. Final achievable tolerances depend on part size and geometry, resin grade, tooling, process control, measurement method, and inspection conditions. Confirm requirements with the molding supplier before tooling release.
A supplier’s sales sheet tells only part of the story. Ask for recent production records showing dimensions, scrap rates, and delivery performance for comparable parts. Request a shop-floor walk-through, even by video. Look for clear maintenance logs and organized material storage. Details matter. Confirm the press has suitable clamping force, shot capacity, and tie-bar spacing for your mold; a large machine is not automatically the right machine. Ask how operators verify resin drying, melt temperature, and mold temperature during each shift. Answers should be specific, not simply “we follow standard practice.”
Review the process evidence from a trial run. Useful records include cycle time, setup conditions, inspection results, and changes made when measurements drift. Ask whether critical dimensions are checked with calibrated tools, and how often those checks occur. One polished sample proves little. A repeat run is more revealing. Capability figures can help, but only when the supplier explains the sample size, measurement method, and production conditions behind them. I would not treat a neat spreadsheet as proof by itself; that is an easy mistake. Notice how the team handles a small problem, too: a delayed measurement or unclear revision can expose gaps in communication. Compare suppliers on documented repeatability, practical equipment fit, and their willingness to discuss limitations plainly.
A supplier’s certificate is a starting point, not proof that every molded part will meet specification. The ISO Survey 2022 recorded more than 1.26 million ISO 9001 certificates across 189 economies. That scale makes certification common, but it does not confirm a factory’s control of your mold, resin, or critical dimensions.
Ask for the actual scope, recent audit findings, and corrective-action records. Paper is not proof.
Review process controls on the production floor. Request a control plan, first-article results, and dimensional data from multiple production runs. For a tight-tolerance housing, check how the supplier tracks cavity-to-cavity variation, machine settings, and resin lot changes.
Plastics Europe’s Plastics—the Fast Facts 2023 reported global plastics production of 400.3 million tonnes in 2022, underscoring the scale of the supply chain. Scale does not remove risk.
Confirm who approves material substitutions, how spare tooling is maintained, and what happens when a press fails. A polished audit can still miss an untested backup plan. Ask for evidence. Review the response, not just the promise.
7 Precision Injection Tips for Buyers in 2026
Comparing Total Costs, Lead Times, and Long-Term Support
A low quotation rarely shows the full investment. Compare tooling, material waste, inspection, packaging, freight, and future design changes. Ask for a cost breakdown with clear assumptions. In production reviews, hidden rework often costs more than the original price difference. Request sample parts, dimensional reports, and process capability data before approval. Real evidence matters.
Tip 1: Confirm the lead time in calendar days. Separate design review, tool fabrication, sampling, corrections, and production. Ask what happens when samples fail inspection. Tip 2: Check capacity during your peak months. A supplier may promise twelve days, then add two weeks during busy periods. That happened to us once. We should have requested a dated production schedule.
Long-term support affects every later batch. Confirm response times, spare mold components, maintenance records, and engineering change procedures. Ask whether process parameters and inspection data remain available after delivery. A reliable partner should explain ownership, storage, and revision control clearly. Do not judge support from one impressive meeting. Test it with a small technical question and measure the reply. Sometimes our own specifications are incomplete, too. Clarifying tolerances early can prevent expensive tool changes and delayed shipments.
Illustrative comparison of three procurement considerations. Cost is shown as a relative index (baseline = 100); lead time is in weeks; support is a buyer-assessment score out of 5. Values are planning examples, not market averages or supplier quotes.
Use these example figures to structure supplier discussions, then replace them with comparable quotations, confirmed production schedules, and documented after-sales commitments.